- Home
- About Us
-
Products
-
Drip Irrigation Pipe Production Line
-
Externally Mounted Pre-Welded Outlet Flexible Pipe Production Line
 Externally Mounted Pre-Welded Outlet Flexible Pipe Production LineRead More
-
Pre-Welded Outlet Flexible Pipe Production Line
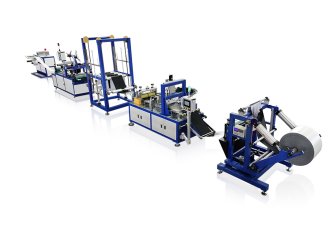 Pre-Welded Outlet Flexible Pipe Production LineRead More
Internally Embedded Pre-Welded Outlet Pipe
Automated irrigation hose production with embedded outlet installation, laser or ultrasonic welding, and adjustable spacing. -
High speed internal flat dripper irrigation pipe production line
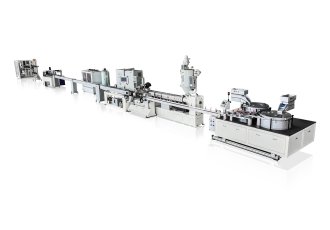 High speed internal flat dripper irrigation pipe production lineRead More
-
High speed thin-wall flat irrigation pipe extrusion line
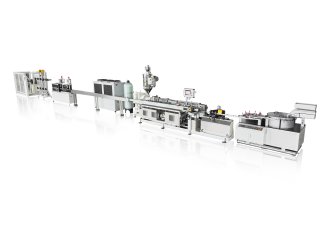 High speed thin-wall flat irrigation pipe extrusion lineRead More
-
High speed cylindrical dripper irrigation pipe machine
 High speed cylindrical dripper irrigation pipe machineRead More
Have a choice for servo drive main motor, Maintenance-free and save electricity about 30%.Design concept of low temperature plasticized method.
-
Pressure Compensating Drip Irrigation Pipe Production Line
 Pressure Compensating Drip Irrigation Pipe Production LineRead More
-
T-tape drip irrigation pipe machine
 T-tape drip irrigation pipe machineRead More
-
round drip irrigation pipe making machine
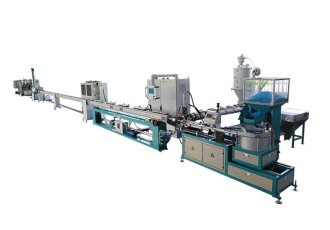 round drip irrigation pipe making machineRead More
-
Flat dripper irrigation pipe making machine
 Flat dripper irrigation pipe making machineRead More
Have a choice for servo drive main motor,Maintenance-free and save electricity about 30%. Design concept of low temperature plasticized method.
-
Labyrinth type drip irrigation pipe production line (One straps four)
 Labyrinth type drip irrigation pipe production line (One straps four)Read More
Wide labyrinth current, the current is turbulence type, multi-water outlet, strong anti-blocking.
-
Externally Mounted Pre-Welded Outlet Flexible Pipe Production Line
-
PET/PP Strap Production Line
-
Heavy PET strapping band production line
 Heavy PET strapping band production lineRead More
PET strapping band, also known as PET plastic belt, is a world widely used new type package material substitute for steel belt.
-
PET strapping extrusion line
 PET strapping extrusion lineRead More
PET strap (plastic steel band) is a high-strength, eco-friendly packaging material widely used as a replacement for steel strapping.
-
PP Strapping Band Extrusion line
 PP Strapping Band Extrusion lineRead More
PP strap with the main material is polypropylene resin, drawing class, because of its plasticity, fracture tensile strength, bending resistance, light weight, easy to use, etc., are processed into the banding has been widely role in various fields.
-
PP Fiber strapping band extrusion machine
 PP Fiber strapping band extrusion machineRead More
-
Fully Automatic PET Strap Winding Machine
 Fully Automatic PET Strap Winding MachineRead More
-
Winder For PP Straps
 Winder For PP StrapsRead More
We can provide automatic winding machine and semi-automatic winding machine.
-
Auto accumulator
 Auto accumulatorRead More
The strap accumulating length more than 70m.
-
PET/PP Monofilament production line
 PET/PP Monofilament production lineRead More
PET/PP Monofilament production line, suitable for the production of raw material pellets or PET bottle flakes recycled materials.can be made into flat or cylindrical monofilament.
-
Heavy PET strapping band production line
-
Plastic sheet production line
-
PC/PMMA sheet production line
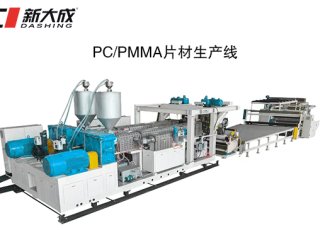 PC/PMMA sheet production lineRead More
-
EVA Solar Film Production Equipment
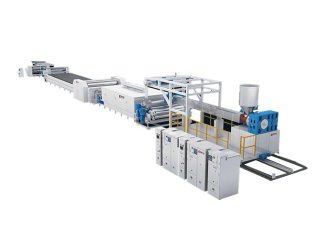 EVA Solar Film Production EquipmentRead More
-
PET/PLA sheet production line
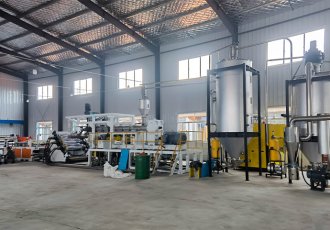 PET/PLA sheet production lineRead More
Single screw or twin screw extrusion technology for choosing.
The PET/PLA sheet production line designed and produced by our company uses parallel twin-screw extruder units, materials without drying crystallization, large output of equipment, low energy consumption, fast production line, high degree of automation, favored by domestic and foreign customers.
-
PVC sheet technology production line
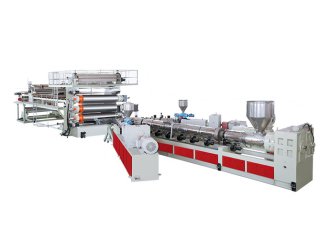 PVC sheet technology production lineRead More
Screw with special mixing and plsticization function.
-
PVC Wave Tile Production Line
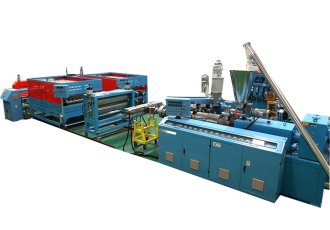 PVC Wave Tile Production LineRead More
The unit is comprised by a twin conical screws extruder SJSZ-65x22 and corresponding wave plate forming machine.
-
Plastic extrusion profile / wood-plastic profile production line
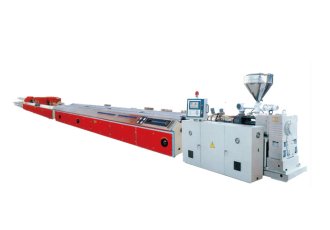 Plastic extrusion profile / wood-plastic profile production lineRead More
The line is the manufacture facilities of PVC plastic profile materials.including window and door series profile, plate, sheet,
-
Plastic extrusion granulation equipment
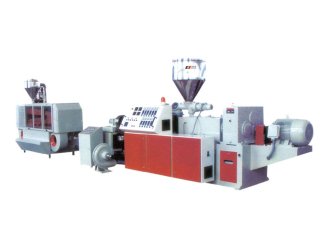 Plastic extrusion granulation equipmentRead More
Made up of Single Screw Extruder or Double Conical Screw Extruder and theirs corresponding auxiliary devices.
-
Twin screw extruder
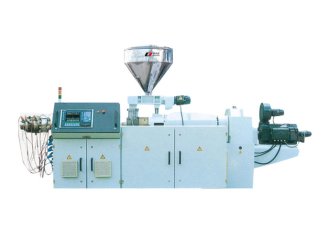 Twin screw extruderRead More
Gentle molding design guarantees the quality of the matter.
-
Plastic mixing unit
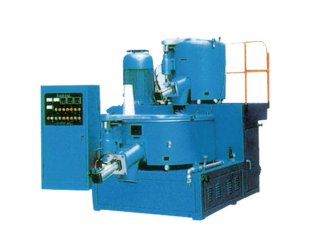 Plastic mixing unitRead More
This unit is developed on the well-developed technique base,chiefly to be used for dry before the engineering plastics processs such as ABS and polycarbonate,and be used for material rationing;blending,coloring and dry of different resin and PEPP and PVC.
-
Pulverizer
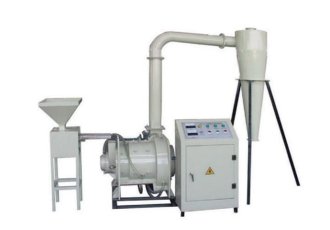 PulverizerRead More
There are all kind of water coding and fan cooling type,shear type plastic and inorganic powder grinding equipments,which can operation continuously under the normal temperature,
-
Plastics crusher
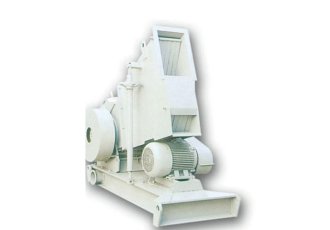 Plastics crusherRead More
SWP series plastics crushers are primarily used to braek up every kind of thermoplastic and rubber,such as plastics profile material tube,stick,silkthread,film,discard old rubber product.The granule provide the extrusion and injection directly.
-
PC/PMMA sheet production line
-
Casting film production line
-
Cpp/cpe casting film production line
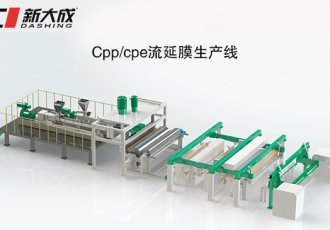 Cpp/cpe casting film production lineRead More
-
PVB/SGP glass interlayer film production line
 PVB/SGP glass interlayer film production lineRead More
-
EVA/POE solar film production line
 EVA/POE solar film production lineRead More
-
TPU casting film production line
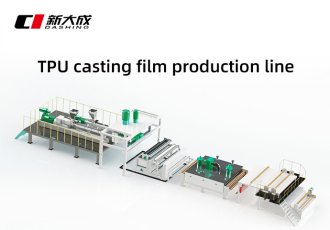 TPU casting film production lineRead More
-
PVDF/ASA casting film production line
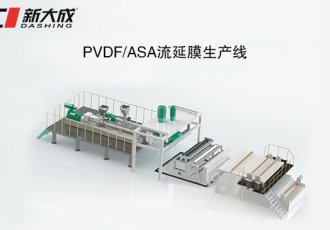 PVDF/ASA casting film production lineRead More
-
Cpp/cpe casting film production line
- Bidirectional stretch film production line
-
Dripper & Inject Mold
-
On-pipe pressure compensated dripper fully automatic assembly
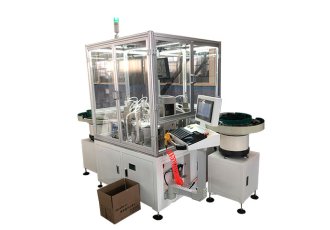 On-pipe pressure compensated dripper fully automatic assemblyRead More
-
In-Line pressure compensated dripper fully automatic assembly
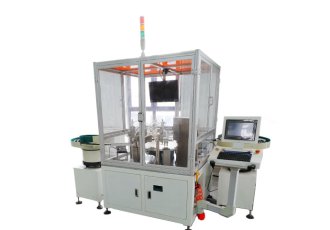 In-Line pressure compensated dripper fully automatic assemblyRead More
I The equipment frame adopts square steel welding, sheet metal door, and the surface is sprayed with plastic; the upper frame adopts aluminum alloy frame, acrylic and aluminum alloy door frame;
-
Flat Dripper Mold
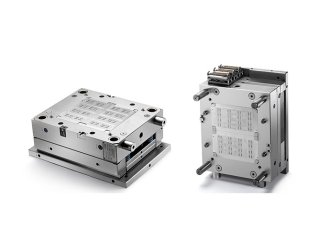 Flat Dripper MoldRead More
-
Cylindrical Dripper Mold
 Cylindrical Dripper MoldRead More
We produce and provide various types of plastic pipe fittings molds.
-
European imports high -efficiency drip emitter
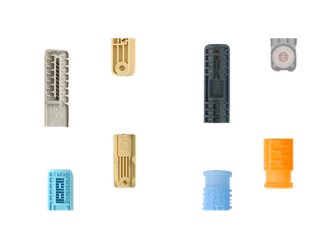 European imports high -efficiency drip emitterRead More
-
Anti -blocking double -hole dripper
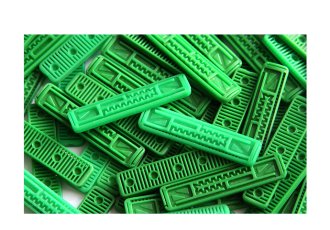 Anti -blocking double -hole dripperRead More
-
Cylinder Dripper (Drip Emitter) & Injection Mold Manufacturer
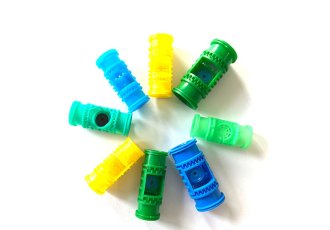 Cylinder Dripper (Drip Emitter) & Injection Mold ManufacturerRead More
XINDACHENG manufactures high-quality cylinder drippers (drip emitters) and precision injection molds for drip irrigation systems. Standard, pressure compensating, and customized solutions are available for agricultural irrigation manufacturers worldwide.
-
Pressure-compensated drip emitter
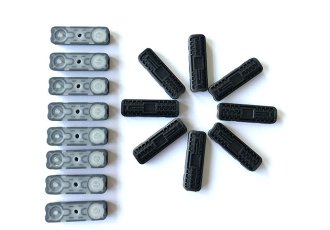 Pressure-compensated drip emitterRead More
-
Drip irrigation tube
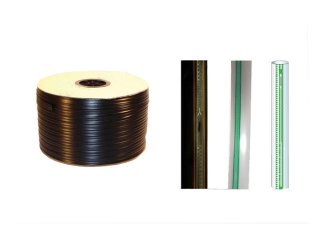 Drip irrigation tubeRead More
-
On-pipe pressure compensated dripper fully automatic assembly
- more
-
Drip Irrigation Pipe Production Line
- Service
- News
- Contacts